

 Français
 Español
 العربية
 한국어

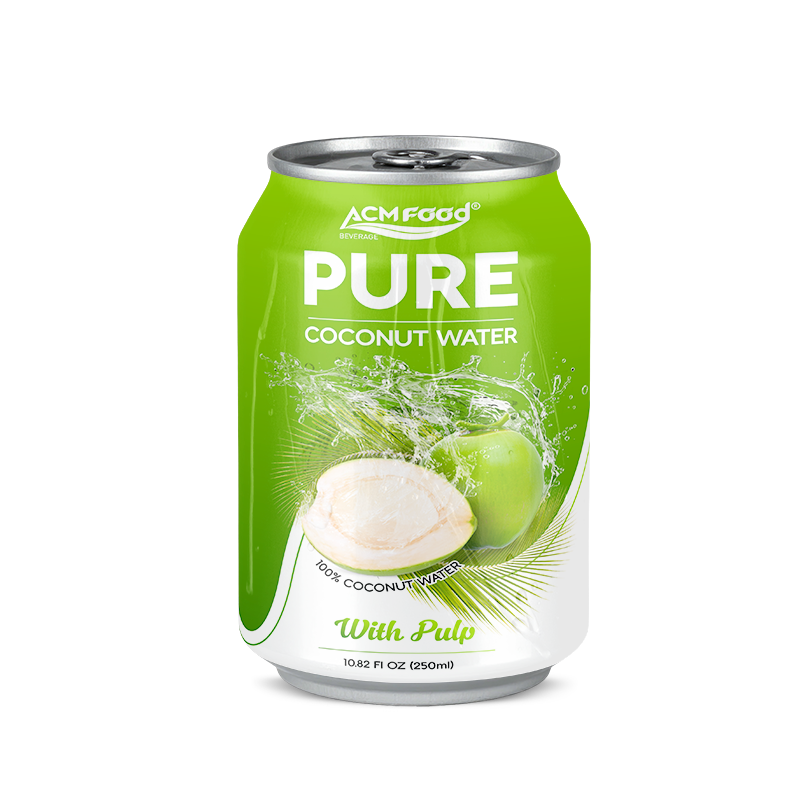
The global beverage distribution landscape faces a critical challenge: balancing authentic product experiences with logistical efficiency. Traditional coconut water packaging often compromises either shelf appeal or supply chain optimization. Our 250ml Alu-can solution directly addresses this gap by combining genuine coconut pulp with a compact short can format designed for modern retail environments.
Modern Coconut Water Distribution Challenges
International distributors encounter specific obstacles when sourcing coconut water products. The delicate balance between preserving natural pulp texture and ensuring packaging durability during transit represents a significant operational hurdle. Many existing solutions either sacrifice authentic mouthfeel for extended shelf life or require excessive packaging that increases shipping costs and environmental impact.
The short can format provides a strategic advantage in this context. Its reduced height compared to standard cans creates space efficiency in shipping containers while maintaining the protective qualities of Alu-can technology. This directly translates to improved cost-per-unit metrics for importers and distributors operating in competitive markets.
Alu-can Technology for Pulp Preservation
Our manufacturing approach focuses on maintaining coconut pulp integrity throughout the production and distribution cycle. The Alu-can construction provides superior barrier protection against light and oxygen exposure, two primary factors that degrade natural coconut pulp texture over time. This technical specification ensures consistent product quality from production facility to retail shelf.
The 250ml volume represents a calculated market positioning. It satisfies single-serving consumption patterns while maintaining competitive pricing structures. For private label partners, this specification allows for flexible branding opportunities across various market segments without requiring packaging redesign for different regional preferences.
Production capacity supports both large-scale export orders and specialized OEM requirements. The manufacturing process incorporates quality control checkpoints specifically designed for pulp-containing beverages, ensuring uniform distribution of coconut particles in every can. This attention to technical detail distinguishes our offering from commodity coconut water products.
Market Application and Expansion Potential
The short can coconut water with pulp serves multiple distribution channels simultaneously. Convenience store networks benefit from the space-efficient packaging that maximizes shelf density. Food service operators appreciate the consistent portion control and easy storage characteristics. Health-focused retail environments value the authentic coconut experience delivered through preserved pulp texture.
Emerging market opportunities in functional beverage categories create additional expansion potential. The natural electrolyte profile of coconut water combined with textural interest from pulp positions this product at the intersection of hydration and sensory experience. Distributors can leverage this dual appeal across traditional and specialty retail environments.
Supply chain integration supports just-in-time delivery models critical for modern distribution operations. The Alu-can packaging withstands varied climate conditions during transit, reducing spoilage rates and improving inventory management efficiency. These operational advantages complement the product’s market appeal for comprehensive distributor support.